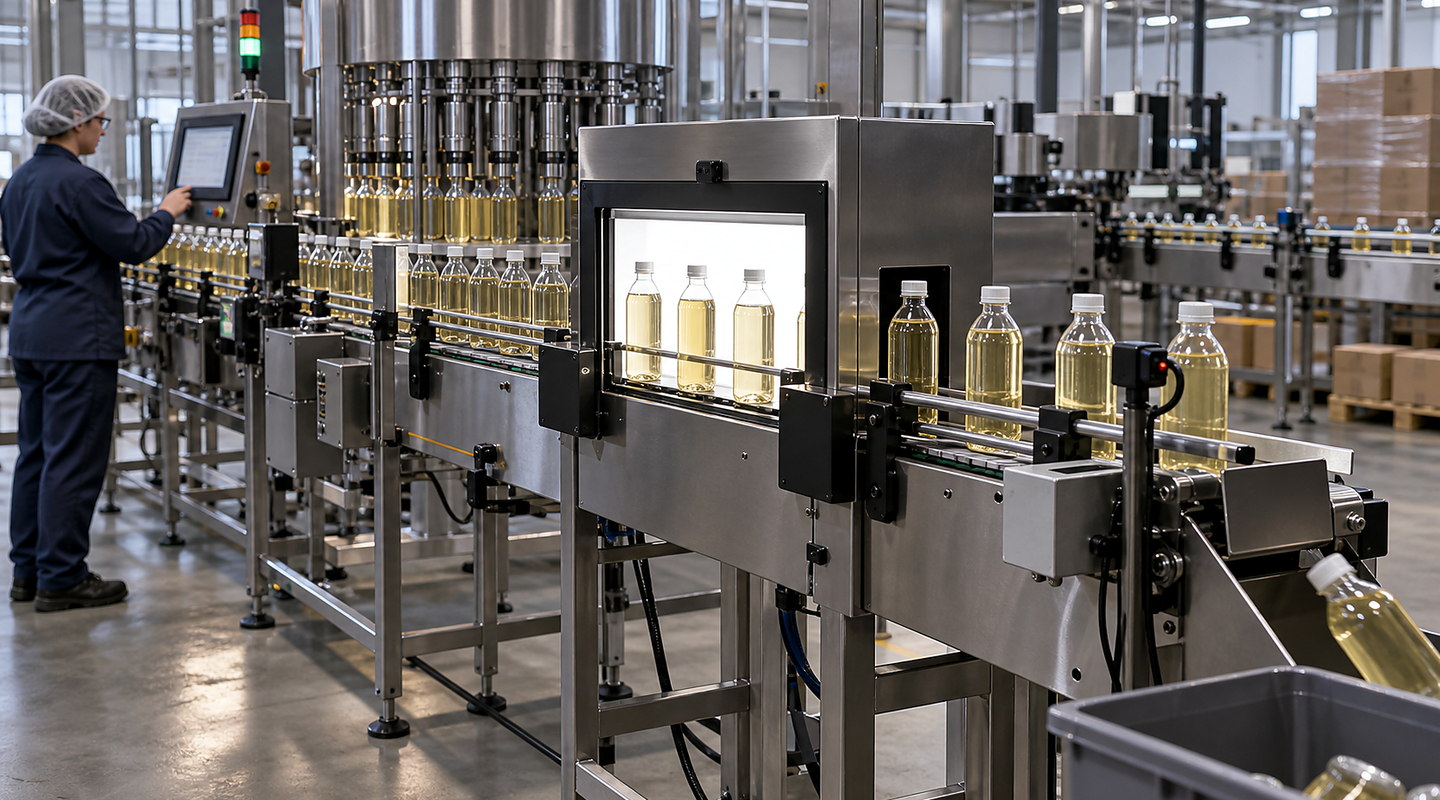
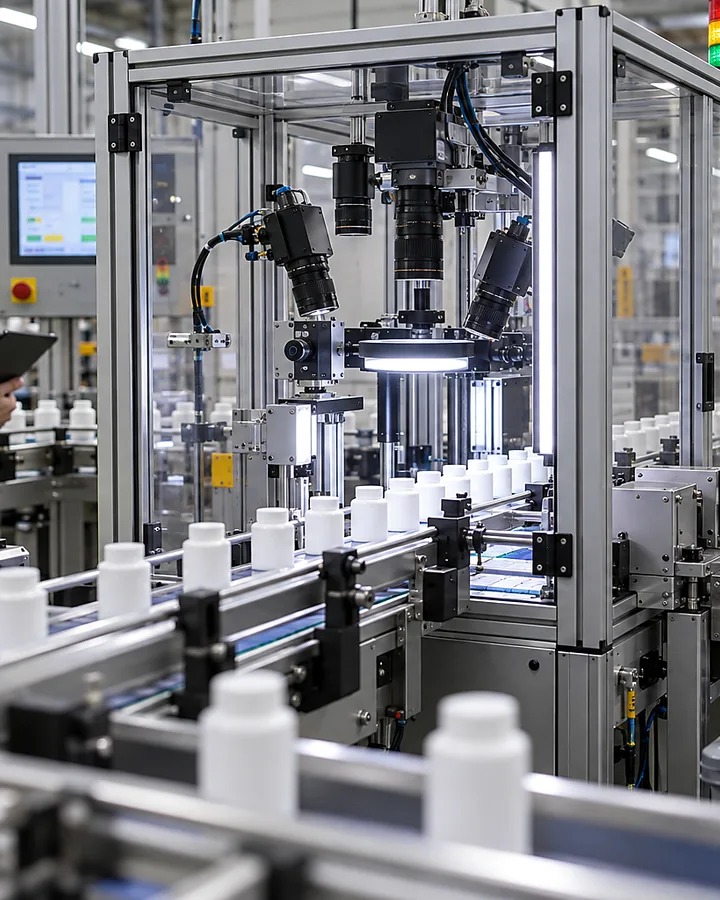
Plan carton checkweighers around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence.
Speak directly with Oxford Vision Systems about carton weight and completeness checks.
Quick answer
Can checkweighing detect the missing contents we are concerned about?
Compare the weight difference caused by the missing item with the normal variation in the complete carton, including packaging. Use representative full and incomplete cartons in a trial at the proposed speed. Agree decision limits, reject confirmation and how uncertain results will be handled before relying on the check.
Six useful questions
Describe what you need from carton checkweighers before choosing a solution
For in-line weight checking of closed cartons, share the normal condition, realistic range and difficult cases the finished system must handle.
Question 1
Carton Contents, Board, Inserts and Carton-to-Carton Tare Variation
Measure the normal weight range of complete cartons, including board, glue, leaflets, inserts and product variation. Supply representative packaging batches and record the carton formats and recipes being compared.
Question 2
Smallest Meaningful Weight Difference and Acceptance Window
Record the weight difference caused by the lightest missing or doubled item and compare it with the complete-carton variation. Agree acceptance limits from representative trials. Weight alone cannot distinguish different contents with equal mass.
Question 3
Pack Dimensions, Stability and Conveyor Presentation
Provide closed-carton dimensions and show flap condition, skew and product movement. Include unstable or marginal examples when reviewing the conveyor presentation and transfers.
Question 4
Line Speed, Spacing, Vibration and Transfer Conditions
State the intended line speed and carton spacing, then review vibration, transfer gaps and changes in pack movement. Trial the actual carton range at the proposed production conditions rather than relying on nominal equipment speed.
Question 5
Reject Device, Removal Confirmation and Reject-Bin State
Define the reject action, physical-removal confirmation and reject-bin states. Agree the production response to a missing confirmation or a bin condition that needs attention. A reject signal alone is not evidence that the carton was removed.
Question 6
Test Packs, Challenge Method, Records and Production Response
Supply known full, incomplete, doubled and marginal cartons from the actual fault list. Agree the challenge method, repetitions, acceptable results, records and production response before accepting the check.
Applications
Two useful starting points for carton checkweighers
The right choice changes with carton contents, board, inserts and carton-to-carton tare variation, smallest meaningful weight difference and acceptance window, your line layout and required results.
Your route from an initial enquiry to a working solution
You can review decisions about reject device, removal confirmation and reject-bin state and test packs, challenge method, records and production response at each stage.
01
Measure Normal Product and Packaging Variation
Share representative packs, measured weight variation and known test packs, including the normal range for carton contents, board, inserts and carton-to-carton tare variation and the difficult smallest meaningful weight difference and acceptance window cases.
02
Trial the Real Pack Range At Intended Line Conditions
Compare suitable methods and use focused trials to show how each option performs against pack dimensions, stability and conveyor presentation.
03
Integrate Transfers, Controls, Rejection and Confirmation
Connect the equipment to your line, services and controls while resolving line speed, spacing, vibration and transfer conditions for day-to-day operation.
04
Challenge Known Weight Faults and Retain Agreed Test Results
Confirm reject device, removal confirmation and reject-bin state, then complete and record test packs, challenge method, records and production response before your operating team takes over.
Important limits
Know what needs a separate check
A checkweigher can only detect a fault that creates a meaningful weight difference.
Normal product and packaging variation must be understood before setting an acceptance window.
A reject signal is not proof that the failed pack was physically removed and confirmed.
Your final solution for carton weight and completeness checks must reflect the law, current standards and site-specific risks that apply to your installation.
Application decision
Will the missing carton item create a clear enough weight difference?
Assess whether carton weight can reveal a missing leaflet, component or pack while allowing for board, glue, inserts and product variation.
Evidence to compare
Compare the lightest missing item with combined carton-board, glue, leaflet, insert and product variation.
Production condition
Explain when weight cannot distinguish two different but equal-mass contents.
Acceptance decision
Direct buyers to vision, code or process checks when mass is not a unique signal.
The quotation brief should record lightest missing or doubled item mass and board, glue, leaflet, insert and product variation. Final suitability remains specific to the samples, line conditions and acceptance tests agreed for your project.